A reliable plywood supplier gives global buyers measurable control over product quality, compliance, delivery, and claims. Buyers should check actual thickness tolerance, veneer structure, moisture level, bonding class, formaldehyde data, batch records, production capacity, packaging, and shipping documents rather than relying on samples alone. EN 636:2012+A1:2015 covers plywood for dry, humid, and exterior conditions, while EN 314-2 sets bonding-quality requirements. For FSC-certified trade, annual surveillance audits are used and FSC certificates are generally valid for 5 years. Reliable supply is repeatable specification control across every shipment.
The first check should be the purchase specification, not the price per sheet. An 18 mm panel can create machining problems when actual thickness changes significantly across one production lot, so buyers often agree measurable tolerances before mass production. The same document should state length, width, number of plies, face and back grade, core species, glue type, sanding, moisture requirements, packing method, and acceptable defects. EN 636:2012+A1:2015 includes requirements covering dimensions, mechanical properties, formaldehyde release, bonding quality, and factory production control.
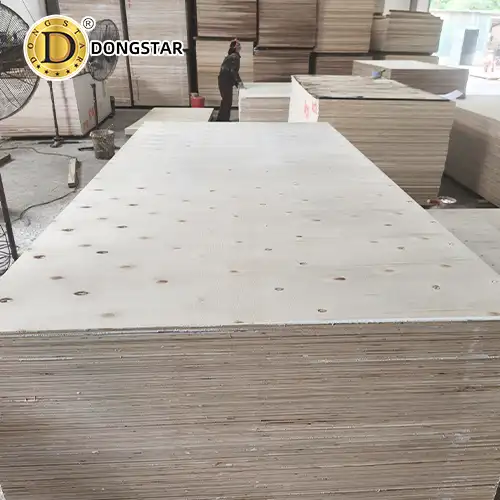
That specification also needs to describe what is inside the panel. Two sheets with the same 2440 × 1220 × 18 mm nominal size may use different veneer species, veneer thicknesses, lay-up structures, and core repairs. A buyer processing 2,000 sheets through CNC equipment will notice variation that may not appear in a 3-sheet sales sample. Open core gaps can affect edge machining, while overlapping veneers can create local thickness changes and uneven surfaces after lamination.
Material control therefore begins at veneer preparation. Factories should sort veneers by species and condition, remove unsuitable areas, dry material before lay-up, and record moisture readings by batch. Instead of accepting “dry veneer” as a description, an importer can request an agreed moisture range and a sampling method, such as readings from 10 or 20 panels selected across several bundles. The agreed range should reflect wood species, manufacturing method, destination climate, and intended use rather than one universal percentage.
Bonding comes next because visual grading says little about what happens between the veneer layers. EN 314-2, first published in 1993, specifies requirements for plywood bonding classes according to end use, with the associated test methods covered by EN 314-1. A supplier should therefore identify the adhesive system, intended service condition, test method, and production batch instead of describing every panel simply as “waterproof.”
A buyer can make the inspection more useful by separating cosmetic and structural checks:
-
Measure thickness at several points rather than at 1 corner.
-
Check 10–20 sheets from different bundle positions instead of consecutive sheets only.
-
Inspect cut edges for gaps, overlaps, missing veneers, and poorly filled areas.
-
Record moisture readings rather than writing only “pass.”
-
Compare face grade against an approved reference sample.
-
Test bonding when the application requires documented performance.
The sample size matters because one approved sheet cannot describe a shipment containing 1,000–3,000 panels. A supplier that records measurements by production date, press cycle, shift, or lot can provide more useful information when a later complaint concerns only several bundles.
Production records also help buyers separate an isolated defect from a larger batch issue. If 24 damaged sheets are reported from a 1,200-sheet shipment, useful records may include the pressing date, adhesive batch, sanding line, packing date, bundle numbers, and inspection results. Without lot identification, both buyer and supplier may have to inspect much more material than necessary.
That level of traceability also supports certification work. FSC Chain of Custody certification verifies how FSC-certified material is identified and controlled through processing and distribution, and the current FSC-STD-40-004 framework applies to sourcing, processing, labeling, and sale of FSC-certified forest products. FSC surveillance is performed annually, while certificates are normally issued on a 5-year cycle.
European construction buyers may also need product documentation related to EN 13986. European Commission documentation identifies EN 13986:2004+A1:2015 for wood-based panels used in construction and lists AVCP System 2+ for relevant structural applications. Buyers should compare the factory name, product scope, intended use, certificate reference, Declaration of Performance, and supplied product instead of treating the presence of a certificate PDF as sufficient.
Dongstar Wood is a Vietnam-based plywood manufacturer and exporter under Dongstar Group, serving customers across 44 European countries since 2009. Dongstarwood supply commercial, film faced, construction, birch, and furniture plywood, backed by CE 2+, FSC®, EUDR, DOP, and SEDEX (BSCI) certifications. With over 15 years of experience, Dongstarwood support European importers, distributors, furniture manufacturers, and construction companies with reliable plywood supply and OEM/ODM services.
Certification, however, does not replace shipment-level inspection. A certificate may confirm that a defined system or product scope has been assessed, while the buyer still needs to verify whether the actual order matches the agreed specification. A professional Plywood Supplier should therefore connect the sales contract, production sheet, inspection record, bundle label, invoice, packing list, and compliance documents to the same product description.
| Area checked | Useful buyer requirement | Why it matters |
|---|---|---|
| Thickness | Measurements across multiple sheets and positions | Reduces machining and assembly variation |
| Core | Agreed species and allowable gaps | Affects edge quality and panel consistency |
| Bonding | Defined adhesive and test requirement | Helps control delamination risk |
| Moisture | Recorded readings from several bundles | Supports dimensional stability |
| Face grade | Approved reference standard | Reduces disputes over visual defects |
| Traceability | Batch or production-date identification | Speeds complaint investigation |
| Packing | Bundle protection and clear labels | Reduces transport and receiving errors |
Production capacity needs similar verification. A factory may state a monthly capacity of 20,000 m³, but that number does not show how much capacity is available for one 18 mm furniture panel, a particular veneer species, or a certified structural product. Buyers should ask for normal output of the exact specification, typical production lead time, peak-season lead time, and which operations are subcontracted.
Order planning becomes more important when ocean freight is involved. A 3-day factory delay can become a longer delivery delay if it causes a container to miss the booked vessel or terminal cut-off. The supplier should therefore work backward from the required loading date and allow time for conditioning, final inspection, packing, container booking, customs documents, and delivery to the port.
Communication during production should use measurable information. “Production is almost finished” gives an importer little planning data. “1,600 of 2,000 sheets are pressed, sanding will finish on September 22, final inspection is scheduled for September 23, and loading is booked for September 25” allows the buyer to coordinate shipping, warehouse space, and customer delivery with dates rather than assumptions.
Packaging then has to preserve the same product quality through several weeks of transport. A 40-foot container can hold thousands of panels depending on dimensions, thickness, density, payload limits, and packing configuration. Bundles may pass through factory forklifts, container loading, port handling, sea transport, destination unloading, and warehouse movement, so edge boards, protective outer sheets, strapping, moisture protection, and readable labels should be agreed before shipment.
Container loading should also be documented. Photos can record container condition before loading, bundle arrangement, package marks, container number, seal number, and the condition of the goods at dispatch. For a mixed order containing 3 thicknesses and 4 panel grades, bundle labels should make each specification identifiable without opening every pack after arrival.
Documentation errors can still delay an otherwise acceptable shipment. Quantities, dimensions, gross and net weight, marks, consignee details, product description, purchase-order references, and container information should match across the commercial invoice, packing list, shipping instructions, and supporting certificates. Checking these fields before departure is usually easier than correcting documents once cargo is already moving between 2 countries.
Supplier performance can then be measured across several orders rather than judged from one delivery. Buyers can record on-time shipment percentage, inspection pass rate, claim quantity, document-error frequency, response time, and repeat defects. For example, 9 on-time shipments from 10 orders give a 90% shipment record; the next review can investigate whether the single delay came from production, documentation, raw material, or shipping arrangements.
Complaints provide another useful test. If 36 panels from a 1,500-sheet shipment show delamination, the supplier should ask for bundle numbers, photographs, storage conditions, defect locations, and affected quantities before reviewing production records. A useful reply explains the investigated cause, identifies the affected lot, proposes a commercial solution where responsibility is established, and records changes for the next production run.
Price comparison should therefore come after specification comparison. A panel quoted 5% below another offer may not be commercially cheaper when thickness, veneer quality, glue, face grade, certification scope, packaging, or allowable defects differ. Buyers comparing 3 quotations should normalize the technical requirements first, then compare price per sheet, cubic meter, or container on the same basis.
For a new supplier, a trial shipment provides more information than another round of samples. A buyer can measure 30 randomly selected panels, record thickness and moisture, cut several sheets to inspect the core, review edge quality after machining, check bundle damage on arrival, and compare shipping documents against the purchase order. Repeating the same inspection method over 3 shipments shows whether production remains consistent when order volume and production dates change.
Reliability is best measured across repeated orders, not one polished sample. A supplier that maintains agreed dimensions, bonding, veneer construction, documentation, traceability, packing, and delivery performance over 6 or 12 months gives an importer far more usable information than one offering a lower quotation with poorly defined specifications.